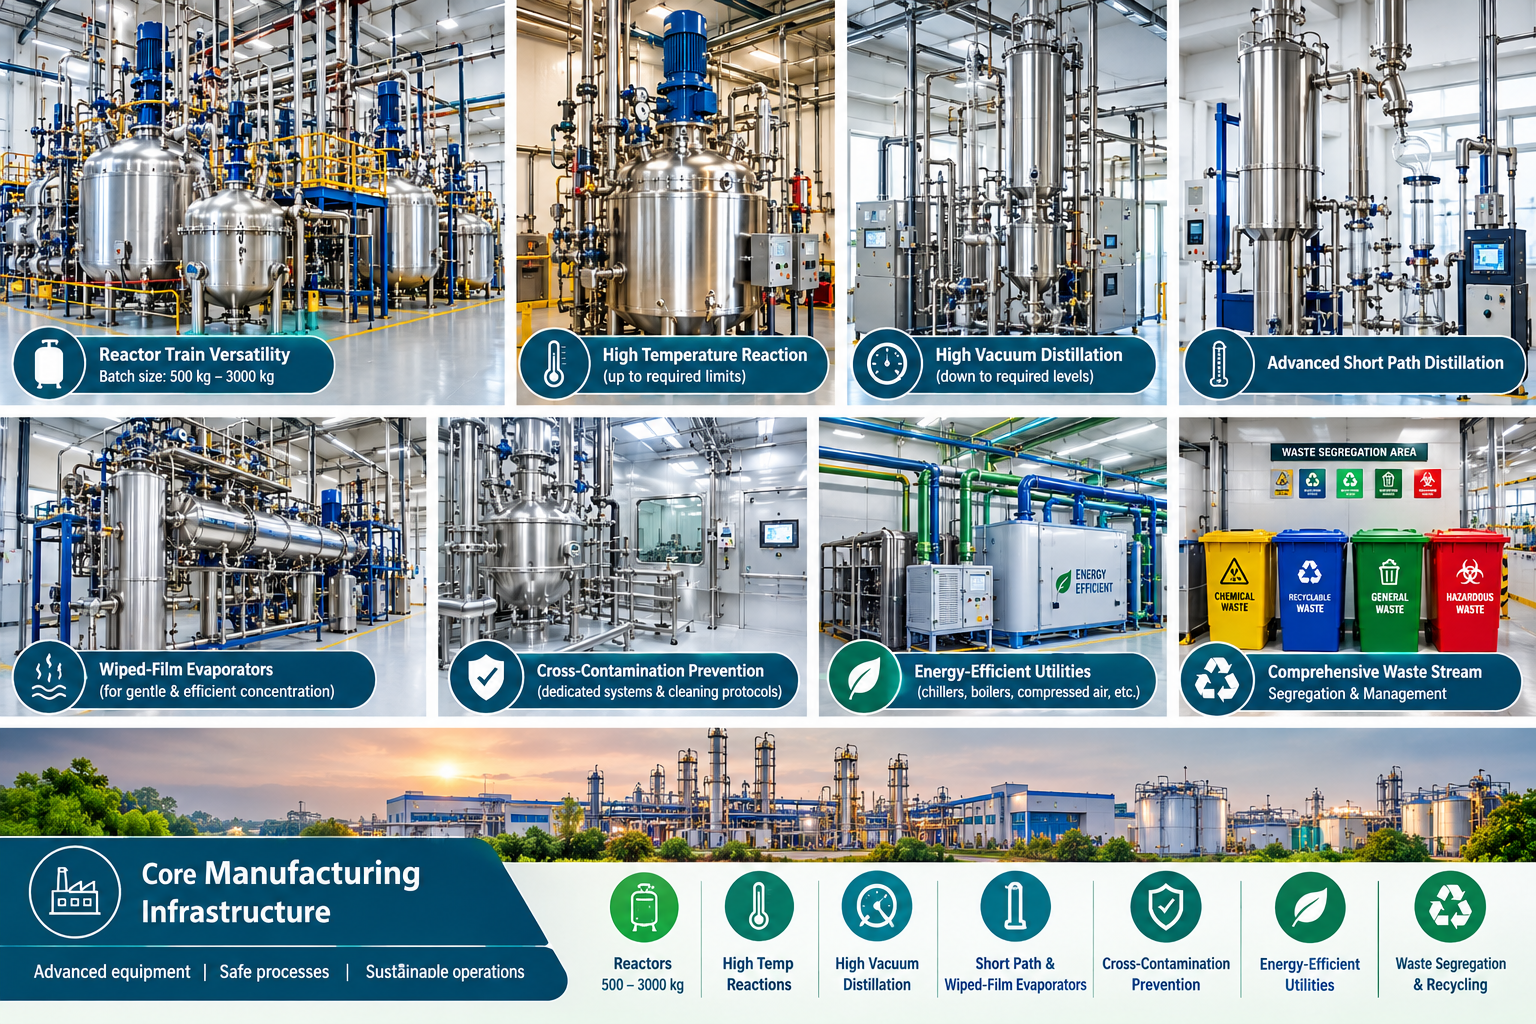
State-of-the-art plant equipped with reactor train versatility, varying in batch size from 500 kg to 3,000 kg with extensive process capabilities — from high-temperature reactions to high-vacuum distillation. Advanced short-path distillation and wiped-film evaporators with strict cross-contamination prevention.
The plant is supported by energy-efficient utilities and comprehensive waste stream segregation.
Our manufacturing facility comprises multiple specialized units — each designed for specific chemical production requirements, with dedicated equipment, controlled environments and established quality processes.
Dedicated manufacturing unit designed for controlled chemical processing, synthesis and production of high-quality chemical products and intermediates. The unit focuses on consistent production, efficient processes and reliable batch-to-batch quality.
Specialized production facility focused on manufacturing specialty chemicals and customized chemical products according to defined technical specifications and customer requirements.
Flexible manufacturing capabilities for customized chemical requirements, allowing production processes to be adapted according to product specifications, batch requirements and customer needs.
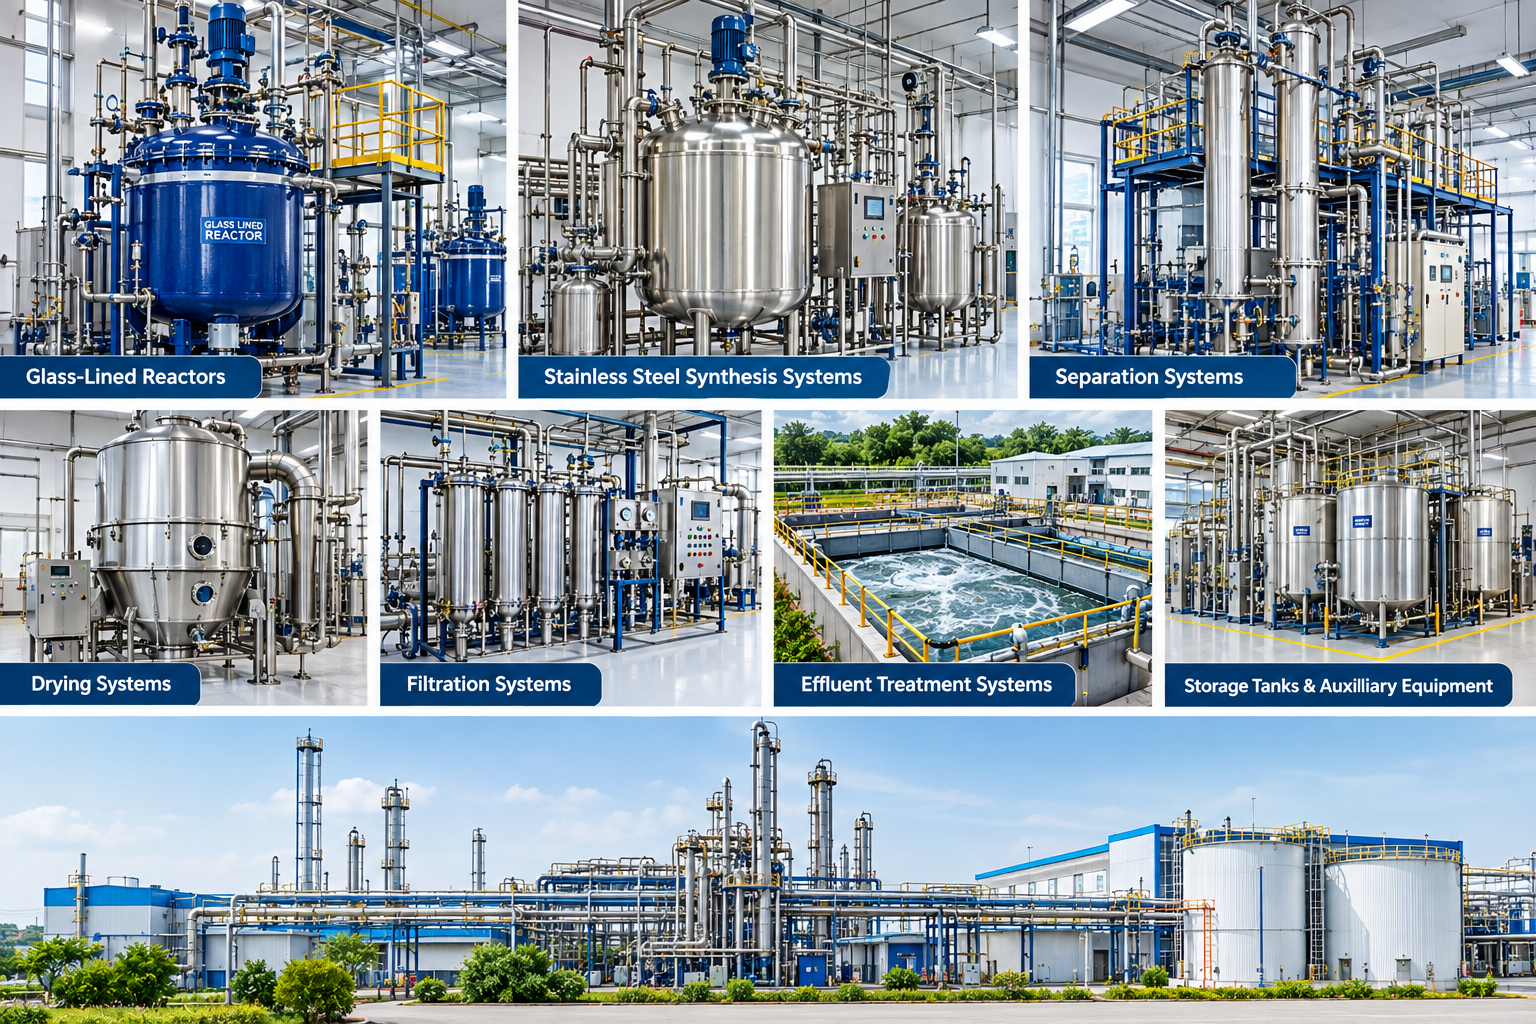
Our manufacturing units are equipped with a comprehensive range of chemical processing equipment — from glass-lined reactors and stainless steel synthesis systems to separation, drying, filtration and effluent treatment systems — enabling reliable production across diverse chemical requirements.
Each facility is designed to handle multi-step synthesis, from small pilot batches to full commercial-scale production, with reactors ranging across multiple capacities to suit varied process needs. Supported by dedicated utilities such as chilled brine, hot oil and steam systems, along with vacuum distillation and centrifuge units, our plants maintain precise control over temperature, pressure and reaction conditions. Strict in-process quality checks, well-maintained cleanrooms and trained technical teams ensure every batch meets consistent standards of purity, safety and regulatory compliance.